Arbor & Taper Chart
Morse, Jacobs and B tapers, 7:24 steep tapers (DIN 2080, SK, BT, CAT), R8, shell mill and horizontal milling arbors, with line drawings.
Download PDF (4 pages, A4)Shop arbors and chucks
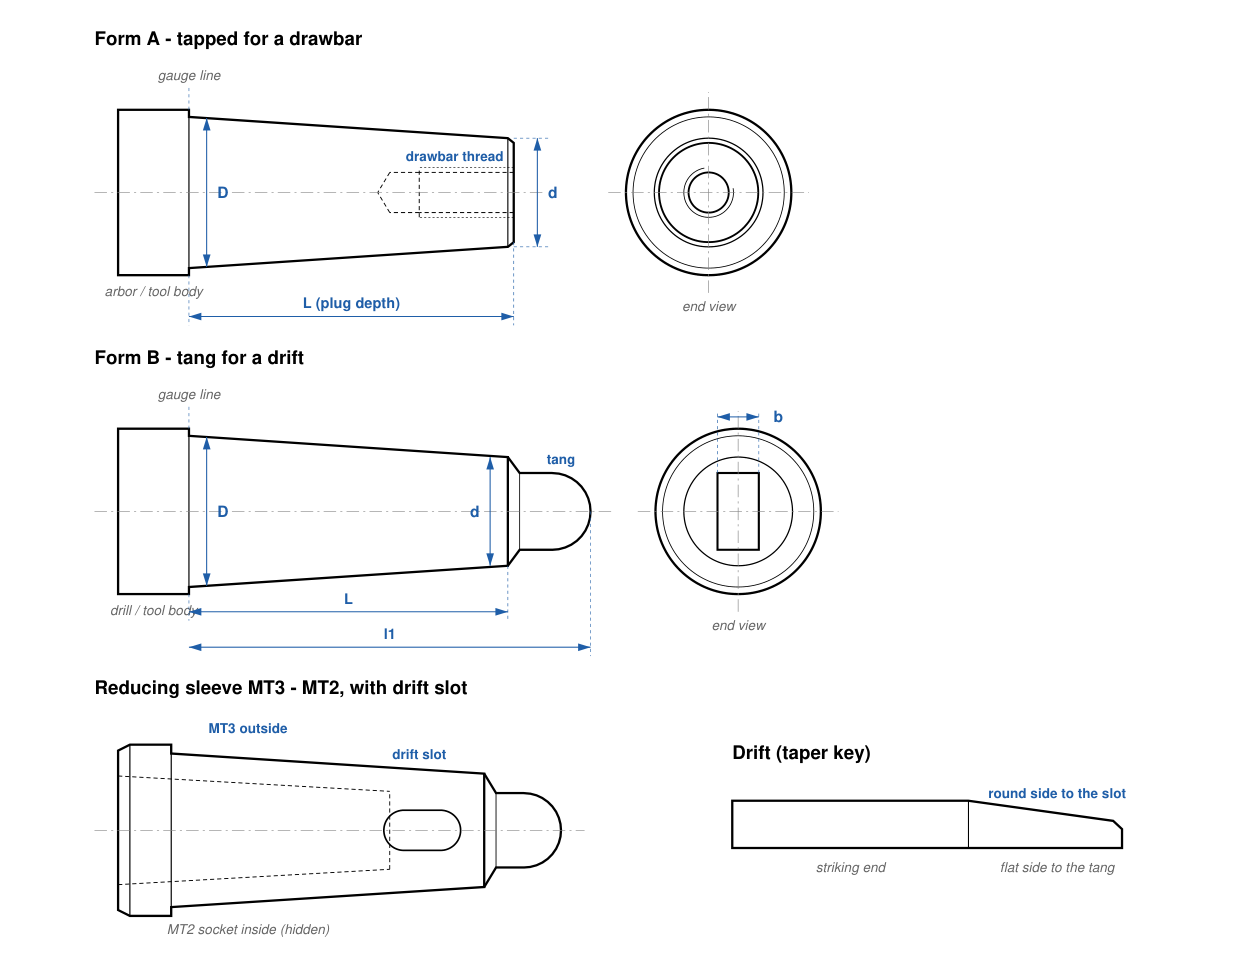
Nominal dimensions for identifying tapers and arbors - not gauging figures. Drawings not to scale; tapers exaggerated for clarity.
Morse tapers (DIN 228)
| Taper | Ratio | D mm | d mm | L mm | D in | d in | L in | Form A thread | Form B tang b mm | Form B l1 mm |
|---|---|---|---|---|---|---|---|---|---|---|
| MT0 | 1:19.212 | 9.045 | 6.40 | 50.8 | 0.3561 | 0.252 | 2.0000 | - | 3.9 | 59.5 |
| MT1 | 1:20.047 | 12.065 | 9.37 | 54.0 | 0.4750 | 0.369 | 2.1250 | M6 | 5.2 | 65.5 |
| MT2 | 1:20.020 | 17.780 | 14.53 | 65.1 | 0.7000 | 0.572 | 2.5625 | M10 | 6.3 | 80.0 |
| MT3 | 1:19.922 | 23.825 | 19.76 | 81.0 | 0.9380 | 0.778 | 3.1875 | M12 | 7.9 | 99.0 |
| MT4 | 1:19.254 | 31.267 | 25.91 | 103.2 | 1.2310 | 1.020 | 4.0625 | M16 | 11.9 | 124.0 |
| MT5 | 1:19.002 | 44.399 | 37.47 | 131.8 | 1.7480 | 1.475 | 5.1875 | M20 | 15.9 | 156.0 |
| MT6 | 1:19.180 | 63.348 | 53.75 | 184.1 | 2.4940 | 2.116 | 7.2500 | M24 | 19.0 | 218.0 |
D - diameter at the gauge line. d - small end. L - plug depth. Form A: drawbar thread. Form B: tang for a drift. To identify a Morse taper, measure the large end (D).
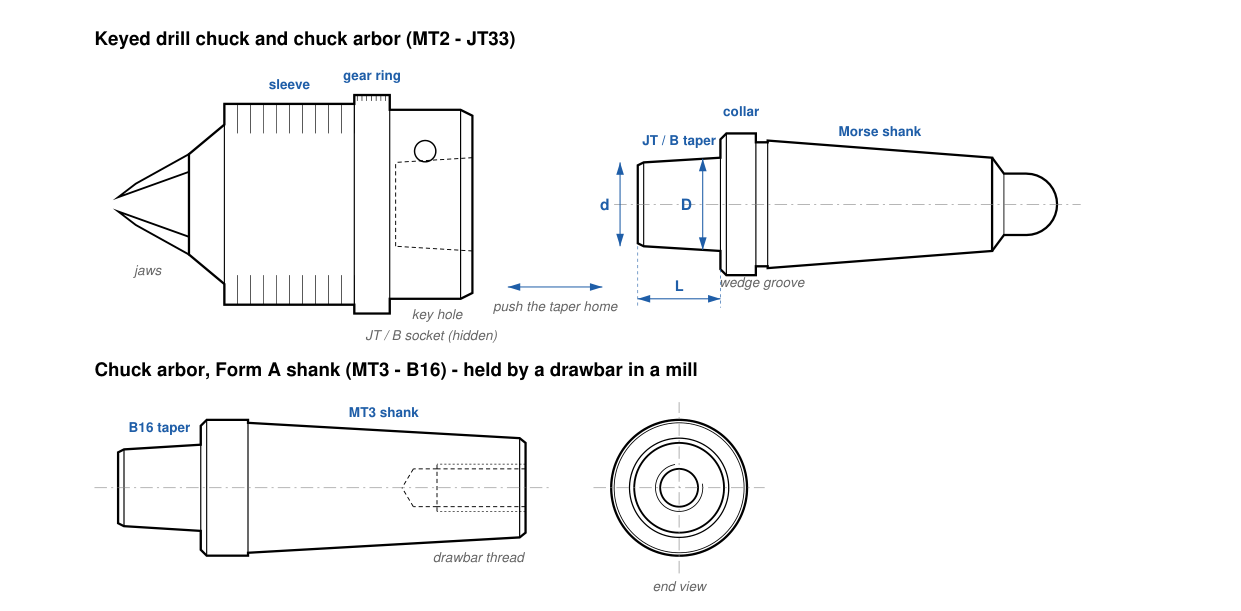
Drill chuck tapers
Jacobs tapers
| Taper | D mm | d mm | L mm | D in | d in | L in |
|---|---|---|---|---|---|---|
| JT0 | 6.350 | 5.802 | 11.11 | 0.2500 | 0.22844 | 0.4375 |
| JT1 | 9.754 | 8.469 | 16.67 | 0.3840 | 0.33341 | 0.6562 |
| JT2 | 14.199 | 12.386 | 22.22 | 0.5590 | 0.48764 | 0.8750 |
| JT2S | 13.940 | 12.386 | 19.05 | 0.5488 | 0.48764 | 0.7500 |
| JT3 | 20.599 | 18.951 | 30.96 | 0.8110 | 0.74610 | 1.2188 |
| JT33 | 15.850 | 14.237 | 25.40 | 0.6240 | 0.56050 | 1.0000 |
| JT4 | 28.550 | 26.345 | 42.07 | 1.1240 | 1.03720 | 1.6563 |
| JT5 | 35.890 | 33.429 | 47.62 | 1.4130 | 1.31610 | 1.8750 |
| JT6 | 17.170 | 15.852 | 25.40 | 0.6760 | 0.62410 | 1.0000 |
B tapers (DIN 238)
| Taper | D mm | d mm | L mm | Ratio | From |
|---|---|---|---|---|---|
| B10 | 10.094 | 9.371 | 14.5 | 1:20.047 | MT1 |
| B12 | 12.065 | 11.142 | 18.5 | 1:20.047 | MT1 |
| B16 | 15.733 | 14.534 | 24.0 | 1:20.020 | MT2 |
| B18 | 17.780 | 16.182 | 32.0 | 1:20.020 | MT2 |
| B22 | 21.793 | 19.760 | 40.5 | 1:19.922 | MT3 |
| B24 | 23.825 | 21.290 | 50.5 | 1:19.922 | MT3 |
An arbor is named shank first, chuck taper second: MT2 - JT33 = Morse 2 shank with a Jacobs 33 chuck taper. B10/B12 come from MT1, B16/B18 from MT2, B22/B24 from MT3.
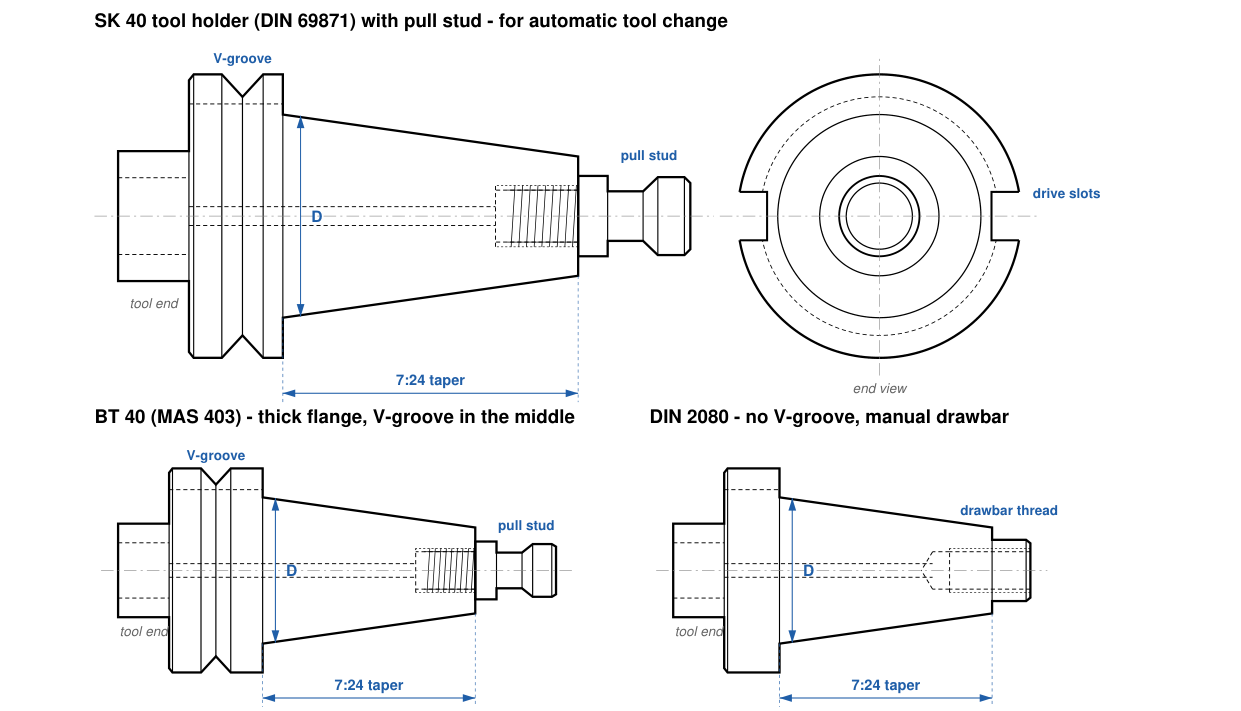
7:24 steep tapers
| Standard | Size | Gauge D mm | Flange mm | Drawbar / pull stud | Notes |
|---|---|---|---|---|---|
| DIN 2080 | 30 | 31.75 | 50 | M12 | Manual drawbar, no V-groove |
| DIN 2080 | 40 | 44.45 | 63 | M16 | Manual drawbar, no V-groove |
| DIN 2080 | 45 | 57.15 | 82.5 | M20 | Manual drawbar, no V-groove |
| DIN 2080 | 50 | 69.85 | 97.5 | M24 | Manual drawbar, no V-groove |
| SK / DIN 69871 | 30 | 31.75 | 50 | M12 | V-flange, pull stud (ATC) |
| SK / DIN 69871 | 40 | 44.45 | 63.55 | M16 | V-flange, pull stud (ATC) |
| SK / DIN 69871 | 45 | 57.15 | 82.55 | M20 | V-flange, pull stud (ATC) |
| SK / DIN 69871 | 50 | 69.85 | 97.5 | M24 | V-flange, pull stud (ATC) |
| BT / MAS 403 | 30 | 31.75 | 46 | M12 | Thicker flange, pull stud |
| BT / MAS 403 | 40 | 44.45 | 63 | M16 | Thicker flange, pull stud |
| BT / MAS 403 | 50 | 69.85 | 100 | M24 | Thicker flange, pull stud |
| CAT / ANSI | 40 | 44.45 | 63.5 | 5/8"-11 UNC | Inch pull-stud thread |
| CAT / ANSI | 50 | 69.85 | 98.4 | 1"-8 UNC | Inch pull-stud thread |
Milling arbors
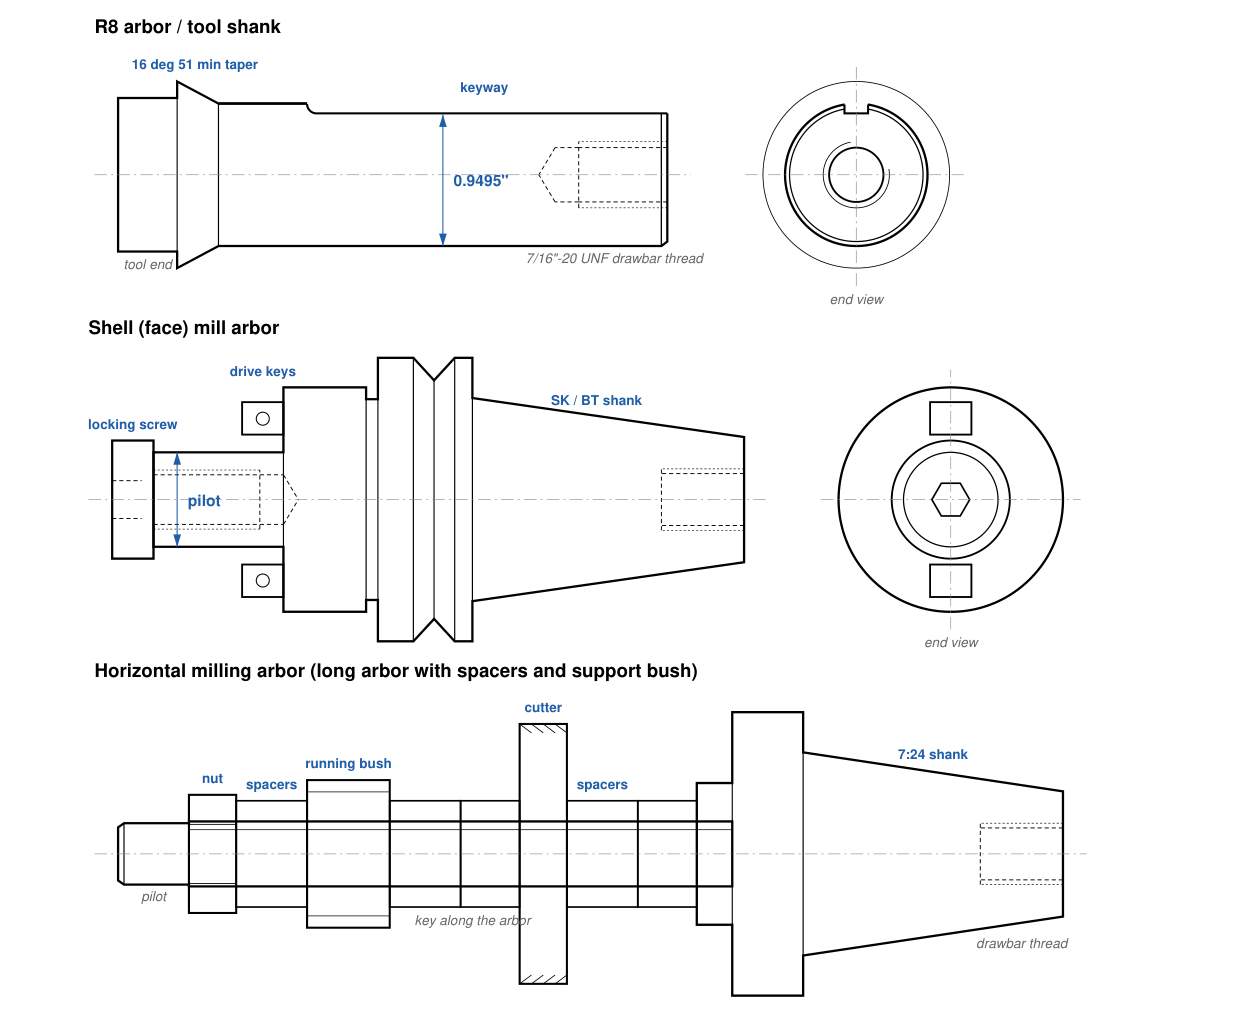
R8 (Bridgeport-type mills)
| Taper | Body dia | Taper angle | Drawbar | Key |
|---|---|---|---|---|
| R8 (Bridgeport) | 0.9495" (24.12 mm) | 16deg 51min included | 7/16"-20 UNF | Keyway in body |
Shell mill arbor pilots
| Pilot dia mm | Typical cutter dia mm |
|---|---|
| 16 | 40 |
| 22 | 50 - 63 |
| 27 | 63 - 80 |
| 32 | 80 - 100 |
| 40 | 100 - 125 |
All 7:24 tapers of one size share the gauge diameter D - the flange, groove and thread tell them apart. SK (DIN 69871) and BT are not interchangeable in an ATC spindle; DIN 2080 holders have no V-groove and use a manual drawbar; CAT uses inch pull-stud threads. Shell mill arbors are named by shank and pilot: SK40 - 27 = SK40 shank, 27 mm pilot. Horizontal milling arbors are sized by arbor diameter (22, 27, 32 mm or 1", 1.1/4") - the cutter bore must match, and the running bush sits in the overarm support.